
Services
Rebar Supply: Cutting, Bending and Delivery That Matches the Pour
Supply is not just getting steel to site. It is getting the right bundles there in the order the crew places them — which is a scheduling decision disguised as a logistics one.
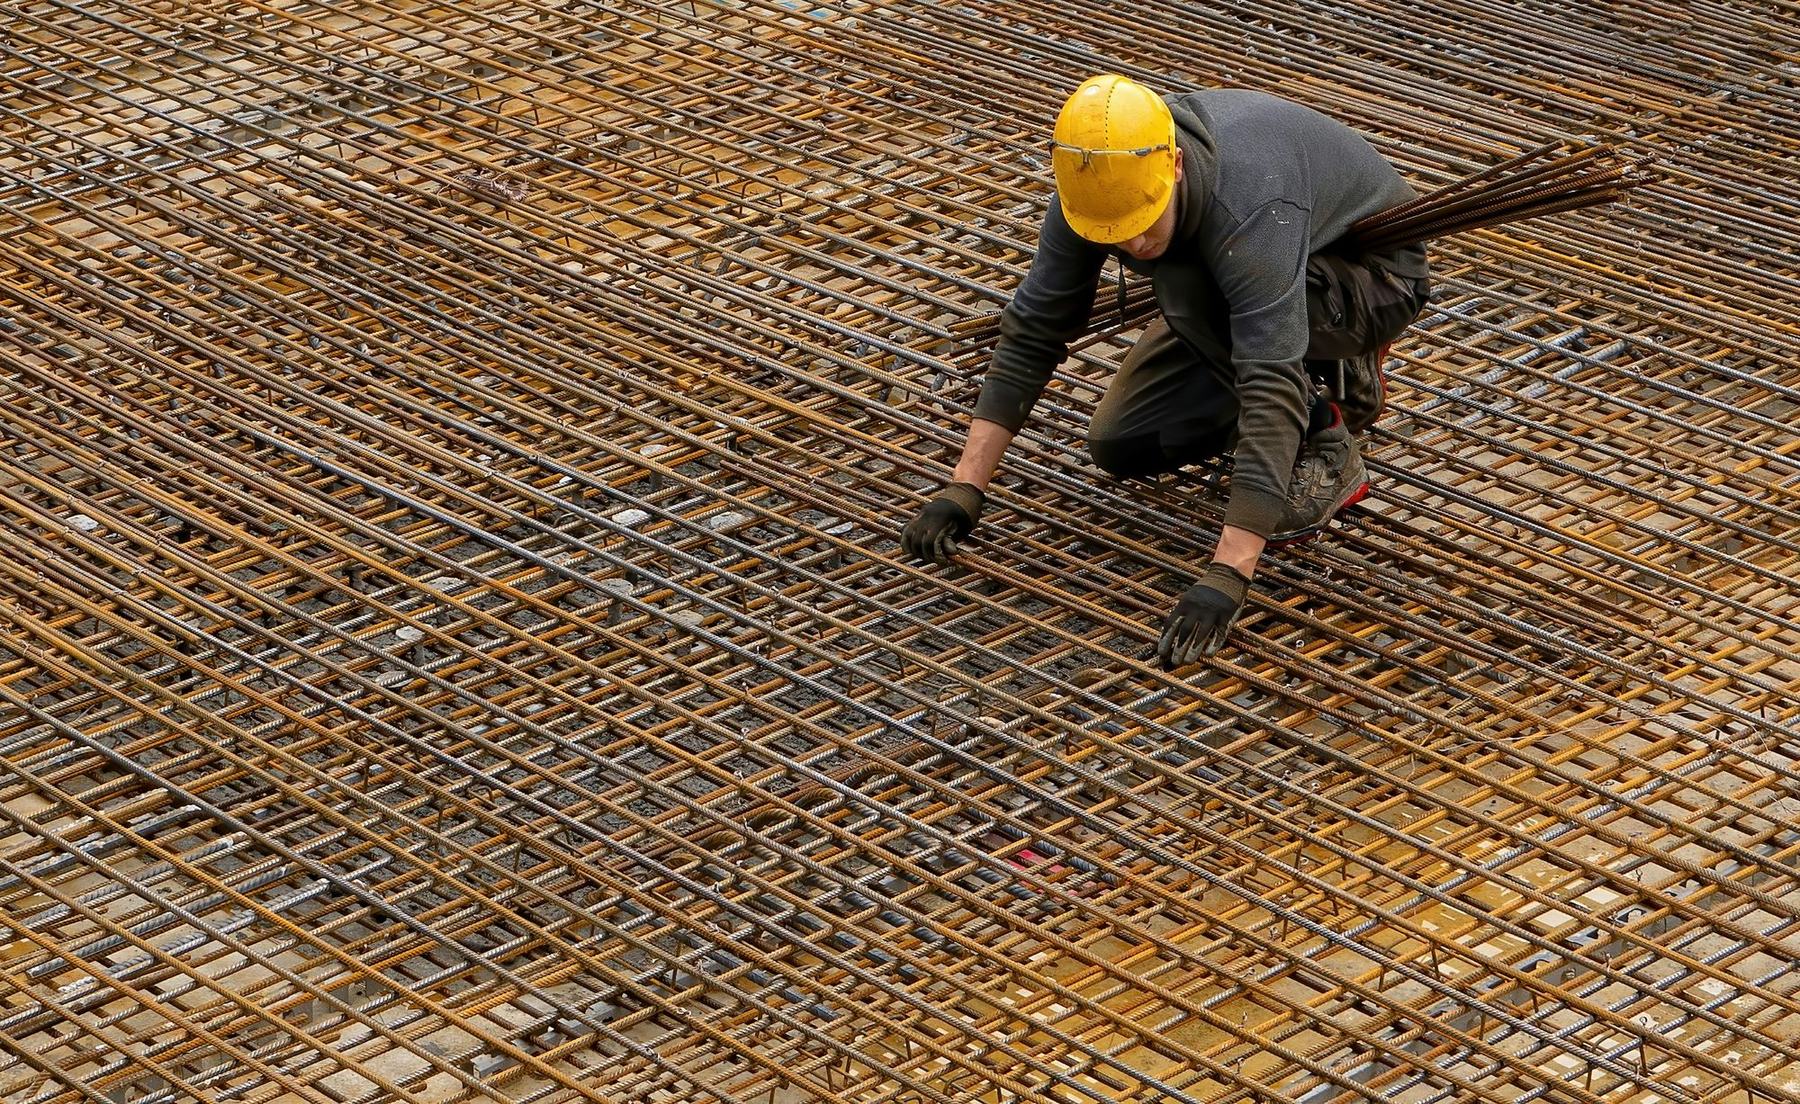
Rucker supplies rebar as well as installing it — cut and bent to spec, delivered to the jobsite. The part worth explaining is what "delivered" has to mean if it is going to help anyone.
Every supplier delivers steel. The variable is whether what arrives is ready to place or is a sorting problem that has been moved from the shop to the site — and that difference is invisible on a purchase order.
Cut and bent to the bar list
Fabricated bar is produced against a bar list generated from the placement drawings: every mark number, its shape, its dimensions, its quantity. Fabricating to the list rather than cutting in the field means less waste, tighter tolerance on bends, and a bundle that can be verified against a tag rather than a tape measure.
Shop bending is also the only way to hold minimum bend diameters reliably, which matters structurally rather than cosmetically: a bar bent too tight is damaged steel, and the tolerance narrows as bar size and grade go up. Field bending has a place for adjustments, not for production.
Bundles that match the sequence
A delivery that arrives as a pile of correct steel in the wrong order is a delivery the crew has to sort before they can start. Bundling and tagging by pour, by element, and by placement sequence turns the same steel into something a crew can work straight off the truck.
- Tagged by mark number, so a bundle is identifiable without unbundling it.
- Sequenced by pour, so the first bundle off is the first bundle needed.
- Sized to the lift, so what comes off the truck can be moved by what is on site.
The third one is the most frequently ignored and the most annoying to discover. A bundle sized for a shop crane and delivered to a site whose largest lift is a telehandler has to be broken down by hand at the gate. On vertical work the constraint is tighter still, because the bundle has to suit the tower crane's available capacity at radius, and crane time is the scarcest resource on a tower.
Sequencing by pour is the one that compounds. Steel loaded so the last bundle off the truck is the first one needed means the whole load is handled twice — once to unload, once to find. Over a job with dozens of deliveries that is a standing tax on the crew, and it never appears as a line item anywhere.
Staging is a site question
Where steel lands is a real constraint on a tight urban site — and getting it wrong means double-handling every bundle. That conversation belongs in pre-construction with the GC, not with a driver at the gate.
The questions are simple and they are cheap to answer early: where can a truck stand, for how long, and can it be unloaded from one side? What is the lift, and what is its capacity at the distance involved? Where can steel sit without being in the way of the next trade, and without being under the formwork that arrives on Thursday? How much can be on site at once?
Answering those in a preconstruction meeting costs an hour. Discovering them at the gate costs the delivery slot, and possibly the pour behind it. This is also why staging assumptions are one of the things that makes two reinforcement bids non-comparable — a bidder who assumed adjacent laydown and one who assumed just-in-time delivery to a kerbside are not pricing the same job.
Storage, weather and coated bar
Steel on site needs to be off the ground and supported so it does not deform, which for long bar means timber at close enough spacing to prevent a sag that becomes permanent.
Ordinary surface rust on black bar is not a defect and does not need removing — a light film actually improves bond. What matters is loose scale and anything that interferes with bond, and contamination such as oil or mud, which does.
Coated bar is a different regime and it starts at delivery: padded slings rather than bare chain, timber between bundles rather than bar on bar, no dragging, and storage out of prolonged sunlight because ultraviolet degrades epoxy. A supplier who delivers coated bar the way they deliver black bar has damaged the product before the crew sees it.
Winter adds its own handling considerations. Bar is unaffected by cold, but ice on bar is a bond problem and has to come off before concrete arrives, and snow in a stored bundle becomes ice in a tied mat. Cold-weather work is mostly a staging and access problem for the reinforcement package rather than a steel problem.
Traceability, where the job requires it
On agency and infrastructure work the tag carries heat identification, and that identity has to survive cutting, bending, bundling and delivery so the steel in the structure can be connected to the mill certificate in the file.
That is an ordinary discipline and it is either in a supplier's process or it is not. It is worth asking about before award rather than at the first submittal, because retrofitting traceability to material already fabricated is not possible.
Why supply and installation together helps
When the same contractor takes off, fabricates and places the steel, the bar list is written by people who know how it will be built. Mark numbers follow the placement sequence, bundle sizes match the lift plan, and a discrepancy between the list and the drawing gets found in the shop instead of on the deck.
It also removes a category of argument. When supply and placement are separate contracts, a bundle that is wrong is a question of whose problem it is, and that question takes longer to settle than the correction would. When they are the same contract, there is nobody to hand it to.
None of that requires the two to be bought together — plenty of jobs separate them for good reasons. It does mean that if they are separate, the sequencing conversation has to happen deliberately between three parties rather than automatically inside one.
If you want steel that arrives in the order your crew will place it, that is a conversation worth having.